
Application Of Mechanical Sealing Technology in The Chemical Industry
The mechanical sealing technology in the chemical industry includes leak free sealing technology, low-temperature sealing technology, ultra-high pressure sealing technology, and lubrication free sealing technology. Most chemical products are toxic, flammable, and explosive. Once a product leak occurs, in addition to causing certain economic losses, it will inevitably cause pollution to the environment and even harm personnel. Due to the characteristics of the above chemical industry, the sealing in chemical equipment must be reliable and have a certain degree of corrosion resistance to ensure long-term use. To meet the complex environment of practical mechanical sealing applications, multiple structures are required Multiple materials and combinations of seals are widely used in the chemical industry, and new processes, concepts, and standards are constantly emerging according to on-site requirements.
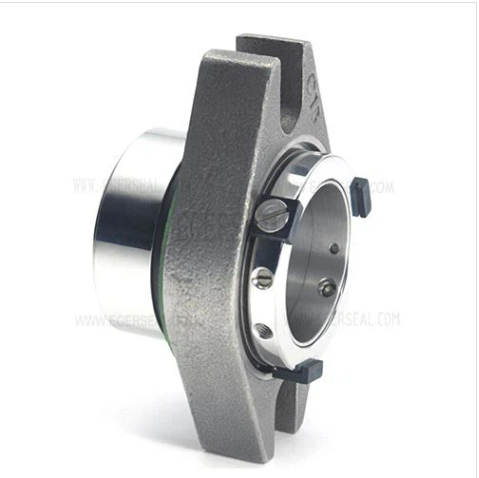
Mechanical seal is one of the most commonly used sealing forms in chemical equipment, characterized by being able to withstand harsh working conditions such as high pressure, high temperature, strong corrosion, and vibration, and having a long service life and low leakage rate. The sealing performance of mechanical seals is closely related to factors such as their structure, materials, processing accuracy, and installation quality. In the chemical industry, mechanical seals are widely used, especially in equipment such as centrifugal pumps, reaction kettles, and refrigerators in the chemical production process. At present, the mechanical seals used in the chemical industry mainly include single end mechanical seals, double end mechanical seals, and corrugated pipe mechanical seals. Among them, bellows mechanical seal is a rapidly developing form of mechanical seal in recent years, with good sealing performance and low leakage rate. It is widely used in corrosive media and high-temperature and high-pressure environments.
With the continuous development of the chemical industry, mechanical sealing technology is also constantly innovating and advancing. In the future, with the increasing demand for equipment reliability and safety in the chemical industry, mechanical sealing technology will face more challenges and opportunities, requiring continuous research, improvement, and innovation to meet the continuous improvement and requirements of sealing performance in the chemical industry.
Need help with seal selection?
Tell us your pump model or working conditions.